
 Cylindrical Cell Machine Line
 18650 Battery Pilot Line
 Pouch Cell Lab. Line
 Prismatic Cell Machine Line

Why Cylindrical Cell Cap Welds Pass Inspection but Leak Anyway
A pilot batch of 21700 cells clears formation and DCIR, and the cap welds look clean under a loupe: smooth bead, no discoloration, no cracks. Then the helium leak station flags four cells, and a teardown of one of them finds a dark speck on the separator that nobody can explain. The speck is weld spatter. The leak is a weld that sealed cosmetically but never penetrated deep enough to close the joint.
Cap welding sits near the end of a cylindrical assembly line, so it gets treated as a formality. It is not. The joint has two jobs at once: it carries the current path and it closes the cell. It can fail at both without showing a visible defect.
The Cap Weld Is a Seal First, a Joint Second
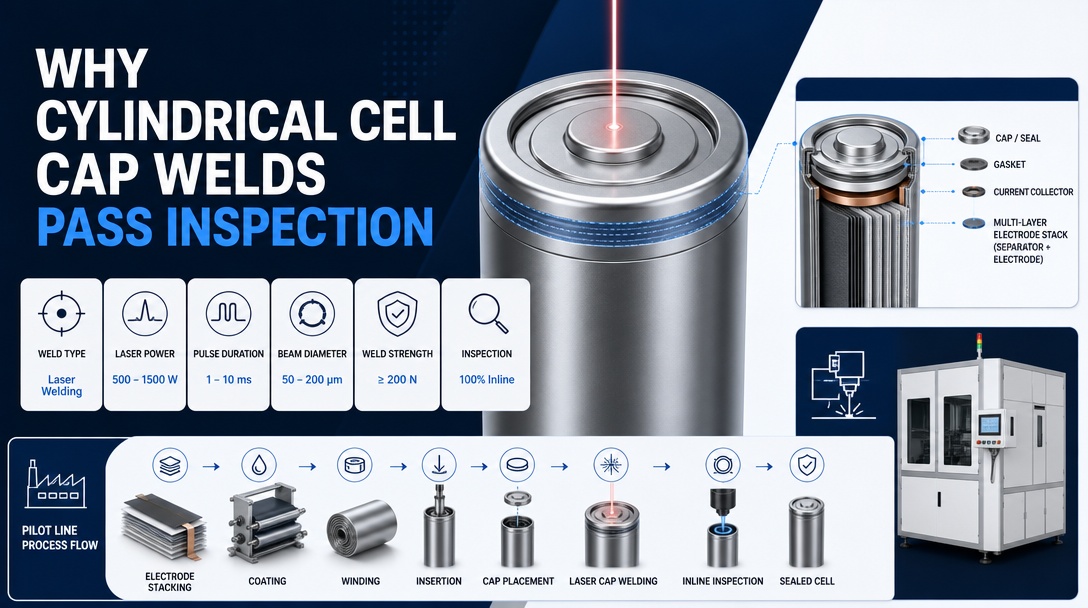
In the standard cylindrical pilot flow — winding, negative tab welding, grooving with adhesive, positive cap welding, baking, electrolyte filling, sealing — the positive cap is normally joined by laser welding. The overall cylindrical battery pilot line setup decides where this step sits and how much room you get for inspection. On Wangsheng's cylindrical pilot lines, this step runs on a dedicated positive-cap laser welder (the MSK-LW-CL200 in the medium-scale line), separate from the ultrasonic machines used for tab welding. That separation is worth copying even if you buy the line elsewhere: a cap weld and a tab weld are not the same problem, and they should not share a machine or an operator habit.
The cap joint has to do two things that pull in opposite directions. As a current path, it wants maximum cross-section and low resistance. As a seal, it wants a continuous, pore-free weld around the circumference. A weld that maximizes one usually compromises the other. A wide, hot bead gives a great current path and a bad seal, because the heat sinks into the can and leaves porosity at the weld root. A narrow, cold bead seals well cosmetically but leaves an incomplete joint that develops a leak under formation pressure or thermal cycling.
That trade-off is the reason cap weld acceptance cannot be a visual check.
Penetration Depth Is the Parameter Nobody Sees
The single most common cap weld failure on pilot lines is not a crack. It is incomplete penetration: the weld root does not reach through the cap material into the can wall, so the joint holds together for handling but is not actually sealed. It can pass a pull-type check because the bonded fraction carries the load. It leaks later because the unbonded root is a capillary path for electrolyte and gas.
Penetration is set by laser power, welding speed, and focus position, and it drifts when any of the three moves. Focus position is the sneaky one. The lens can sit at the same dial reading while the stack-up of cap and can changes by a few tenths of a millimeter between suppliers, moving the beam focus away from the joint interface. The result is a batch of welds that look identical and leak at different rates.
The practical pilot-line habit is to cross-section a sample cap weld before each batch, not to trust the machine display. Cut through the weld, etch lightly, and look at the root under magnification. You are checking one thing: whether the weld root reaches the can wall across the full circumference, not just at the start and end of the weld.
Spatter Is Contamination, Not Cosmetic
Laser welding throws molten metal. On a closed cell, that metal has exactly one place to go: inside. Spatter particles land on the separator, the electrode edge, or the cap interior. Most are harmless. One particle in the wrong place — a conductive speck bridging the positive cap and the can edge, or sitting on a thin separator area — is a micro-short that shows up weeks later as self-discharge or a failed aging check.
Pilot lines see this as a mystery because the weld looks fine and the electrical test that catches it happens much later. The teardown in the opening example is typical: the failure is found by looking, not by testing.
Spatter control is a process decision, not a cleaning step. Shielding gas flow, weld speed, and the joint fit-up decide how much spatter is generated. A cap that sits flush on the can produces far less spatter than one with a visible gap, because the gap lets the beam keyhole fluctuate. When a line starts seeing spatter, the first checks are joint fit-up and shielding gas coverage, not laser power.
Aluminum, Steel, and Copper Each Need a Different Recipe
Cylindrical cap assemblies mix materials, and the laser recipe has to follow the material. Steel caps weld with a forgiving window. Aluminum caps are the opposite: aluminum's oxide layer, reflectivity, and thermal conductivity make the process window narrow, and the weld is prone to porosity and hot cracking. Copper, used on some high-rate designs, is the hardest of the three because it reflects most of the beam energy until it melts.
The mistake is carrying one recipe across materials. A steel recipe run on an aluminum cap produces a weld that looks acceptable and leaks by the next day. The fix is not more power; it is a separate qualification run for each cap material, with its own cross-section and leak samples.
For dissimilar joints — a nickel-plated steel cap over an aluminum tab, for example — the interface can grow brittle intermetallic layers over time. The weld can pass every initial check and degrade in storage. If your design mixes metals at the cap, the qualification plan should include a storage or aging leg, not just a fresh-weld test.
How to Qualify Cap Welds on a Pilot Line
A workable acceptance sequence for cylindrical cap welds looks like this:
- Cross-section one weld per batch before sealing: check root penetration and porosity.
- Leak-check every sealed cell after welding — on pilot lines this usually means a helium leak station for the cells that carry a leak spec.
- Hold a few samples from each batch for a storage leg: recheck weight and DCIR after two to four weeks.
- When the cap supplier, can supplier, or material changes, repeat steps 1 and 3 even if the machine settings have not moved.
At the same time, ask the supplier three questions before you order a cap laser welder. What is the focus position tolerance over a full shift? What shielding gas setup does the machine ship with, and what gas flow range does the recipe support? And can the machine log weld energy per cell, the way a tab welder should? If the answer to the third one is no, you will be debugging cap welds with no data.
When the Cap Weld Is Not the Problem
Not every leak after sealing is a laser weld. The crimp seal around the cap — groove depth, crimp height, gasket compression — fails on its own timeline, usually after formation rather than at the sealer. If the leak pattern tracks the crimp station rather than the laser welder, walk the mechanical seal path before touching the laser recipe. The two failure modes need different fixes, and changing laser power to fix a crimp problem wastes a batch and hides the real cause.
Cap welding deserves the same respect as tab welding: a small joint, a narrow process window, and a failure that shows up late. If you are setting up a cylindrical pilot line, treat the cap weld as a qualification step with its own samples, its own leak check, and its own recipe per material. The cell that leaks at aging will thank you — or rather, the batch that does not leak will.
For a line that needs a cap welding step sized to pilot volumes, Wangsheng supplies positive-cap laser welders, like the battery cap cover laser welding machine for cylindrical and prismatic cells, integrated into the line flow. Contact Wangsheng to discuss the qualification setup for your cell format.