
 Cylindrical Cell Machine Line
 18650 Battery Pilot Line
 Pouch Cell Lab. Line
 Prismatic Cell Machine Line

When Do You Really Accept a Battery Pilot Line?
Signing the acceptance certificate on the day the last crate is unpacked feels efficient. Three months later, when the first electrode batches still cannot hold coating weight across the web, the same signature reads differently. It says the line met its acceptance criteria, the supplier's engineers are already on another project, and the problem is yours. That is the real cost of confusing "delivered" with "qualified."
A pilot line is not a machine; it is a process that happens to live inside machines. Acceptance is not the moment the paperwork is signed. It is the moment the line repeats a batch within the tolerances you wrote into the purchase order. Getting there takes three distinct checkpoints: factory acceptance testing at the supplier's site, site acceptance testing after installation, and a ramp period you should treat as part of the contract, not as a favor.
FAT: Fix It Where Labor Is Cheap
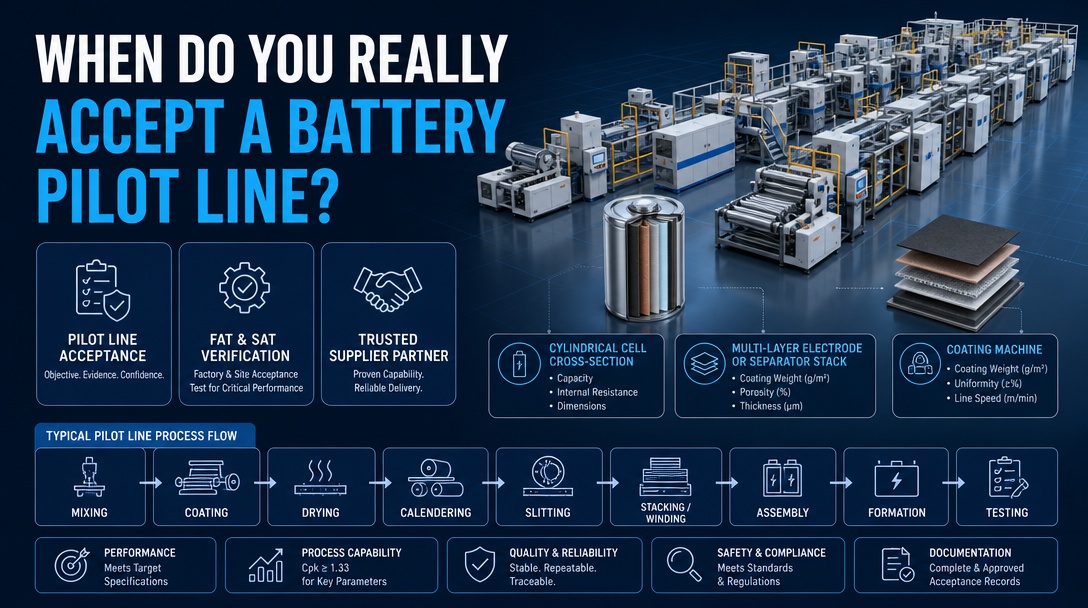
The factory acceptance test is the cheapest place to find problems, because everything is still in the supplier's building, with their tooling, their electricians, and their schedule pressure. Treat it as a rehearsal of your process, not a tour.
Bring your own checklist and your own material list. Run the line empty first, then with dummy material. Time the changeover between your formats with a stopwatch; the number in the quotation is usually optimistic. On a cylindrical line, that means asking for a real changeover from 18650 to 21700 tooling while you watch. On a coating line, run a test web at your target width and coating speed, then weigh samples across the web and compare the spread with the specification. The tolerance levels we quote on our battery coating machine pages should be the same numbers that appear in your FAT report.
Safety interlocks get tested last by most visitors, which is backwards. Every interlock that is hard to reach is one an operator will bypass in month two. Test them all, including the ones the supplier says "nobody ever triggers."
SAT: Installed Is Not Qualified
Site acceptance starts after installation and leveling, and the common failure is compressing the timeline. The line is assembled, the utilities are connected, and someone suggests running real electrodes on day one. Do not. Run the sequence: dry cycle, dummy run, sacrificial material, and only then your real electrode stock.
The first two weeks on site decide more about the line's first year than any other period. Watch the operators the supplier's engineers trained; what they do without prompting tells you whether the training took. Measure everything the acceptance criteria name, and also the things they do not: scrap in the first batch, setup time between jobs, and how long a jam takes to clear.
The Checklist Items Everyone Skips
Three categories of acceptance items routinely get signed off without being verified:
- Spare and wear parts. Confirm the list, the prices, and the lead time. When a coating head or a crimping die wears out, the line stops until the part arrives. A 45-day average lead time for standard parts is normal in this industry, which is why Wangsheng pushes customers to lock the spares list at acceptance instead of discovering it during the first breakdown.
- Documentation. Calibration certificates for every measuring instrument, the electrical drawings as built, the CE declaration where applicable, and the software versions. None of this is interesting, and all of it is hard to get later.
- The response commitment, in writing. A pilot line always breaks during a trial window. What matters is not the brochure promise but the contract line: how fast the supplier responds, and how fast a technician can be on site. At Wangsheng we hold ourselves to a two-hour response and 24-hour on-site service for emergencies, and that commitment belongs in the acceptance paperwork, not in a sales slide.
Questions That Separate a Supplier From a Vendor
Any supplier can assemble a line. The difference shows up in the answers to four questions, and all four should be asked before the purchase order, then re-verified at acceptance:
- What happens to the acceptance criteria if your process changes? If you switch from wet to dry electrode, or add a cell format, does the line have spare capacity, or is it built exactly to today's specification?
- Who runs the ramp, and for how long? A line that qualifies in the supplier's factory can still fail on your floor because of utilities, operator skill, or material variation. The ramp period is where pilot line process stage matching actually gets tested.
- What do you do when a target is not met at SAT? The answer you want is a defined retest procedure with a deadline, not a promise to "look into it."
- What is not included? Consumables, training days, tooling for additional formats, installation supervision. List everything that is extra, because the gap between the quoted price and the working line is usually a list.
When You Should Not Sign
Hold the signature when any of these is true: the acceptance criteria in the test report do not match the purchase order; safety issues remain open; the spare parts list is not finalized; or the training record does not match the operators who will actually run the line. Partial acceptance is a legitimate tool. Accept the line, list the open items with dates, and tie the final payment to the last item, not the first. Knowing when not to accept is worth more than any warranty clause, because a signature is a statement that the risk belongs to you now.
The best time to decide what acceptance means is before the purchase order, because that is when the supplier will agree to the most. The second best time is at FAT, when fixing a problem costs a week instead of a quarter. By the time the crates arrive, the checklist is mostly written. Make sure it is yours.
When you spec your next cylindrical battery pilot line, ask the supplier to put the commissioning procedure in the contract, with the FAT and SAT criteria attached. If you want a reference for how that looks in practice, contact Wangsheng and we will walk you through our FAT/SAT protocol before you commit to anything.